Control sweater delivery by fixing one purchase-order quantity for every style, color and size, then stating whether tolerance applies per SKU, per color or only to the total. Keep production allowance separate from billable delivery. Before shipment, reconcile first-quality packed units, rejects, repairs, samples and any approved variance. Never assume a universal percentage or replace a missing size with extra units of another size.
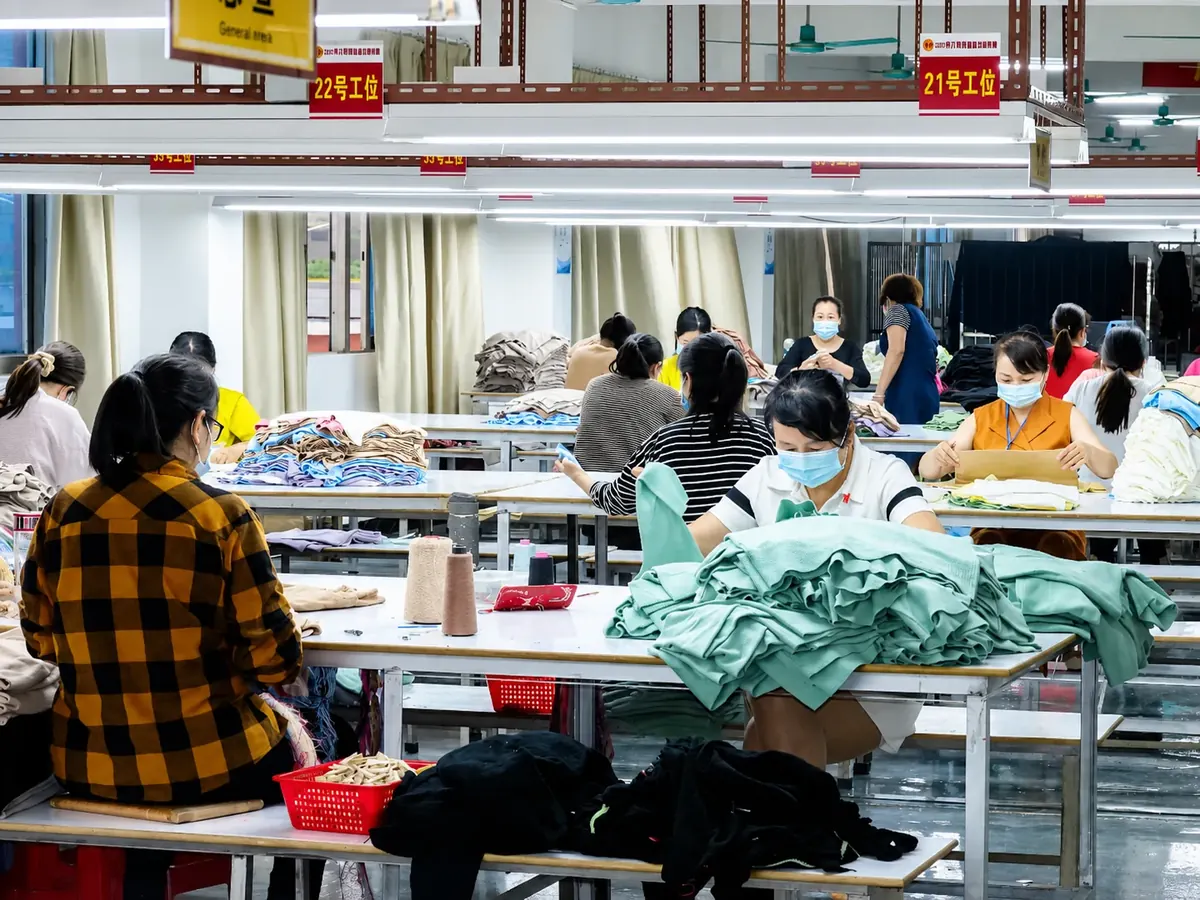
Turn the assortment into controlled PO lines
Write a separate line for each style, color, size and destination combination. Include the buyer SKU, supplier style, color reference, size, ordered units, unit price, delivery window and pack route. If one color uses two labels or markets, separate those variants too. A headline order of “1,000 sweaters” cannot tell production or the warehouse which units are missing.
GS1's apparel guidance treats size and color as product variants that may require distinct identification. Whether or not your business uses GTINs, the operating principle is useful: every sellable variant needs an unambiguous identity across the PO, labels, packing list, carton marks and receiving system.
| Control point | Write explicitly | Risk if omitted |
|---|---|---|
| Quantity basis | Per SKU, color subtotal and order total | Extras hide a shortage elsewhere |
| Tolerance | Exact, or named level and boundary | Unapproved over- or under-shipment |
| Quality basis | Accepted first-quality packed units | Rejects counted as deliverable |
| Assortment | Units per size in each carton | Receiving and allocation errors |
| Variance approval | Authorized person and deadline | Factory ships before buyer decision |
| Documents | PO, final count, packing list and invoice | Conflicting commercial records |
State where tolerance applies
There is no universal sweater-delivery tolerance. The PO should say “exact quantity” or define the permitted variance and its level. A tolerance on the grand total does not automatically permit a shortage in XS to be offset by extra M. Likewise, a color-level tolerance does not authorize changing the approved size ratio.
Define whether the boundary is bilateral or only allows a shortage, how rounding is handled, whether the buyer must approve every variance, which units are billable and whether different rules apply to core and fringe sizes. If a contract, letter of credit or retailer manual also controls quantity, reconcile its wording with the PO through qualified commercial review.
Separate production allowance from delivered quantity
A manufacturer may plan extra panels or garments to cover setup, destructive tests, defects and repair risk. That is a production decision, not automatic permission to invoice and ship every extra unit. State whether production allowance is included in price and what happens to unused first-quality units, seconds, branded rejects and leftover labels.
Protect brand control without inventing ownership terms. Agree in writing who may authorize extra finished goods, whether logos must be removed from rejected units, how destruction or disposal is evidenced and whether any retained reserve can support an approved replacement. Local law and the signed contract govern enforceability.
Freeze the size ratio before material commitment
Build the ratio from the buyer's demand evidence—historical sales, preorders, wholesale allocations or a documented launch assumption. Convert percentages into whole units and show the rounding rule. Confirm that every color subtotal equals its PO quantity before the factory books yarn or labels.
Do not use an equal XS–XL split by default or borrow another brand's ratio. A ratio describes commercial demand; it does not replace an approved grade rule or size set. If the buyer changes the ratio after yarn, labels or packing materials are committed, assess material use, production sequence, carton plan, cost and delivery before approval.
Count only accepted first-quality units
Define the deliverable quantity as finished, inspected, correctly labeled and correctly packed first-quality units unless the contract says otherwise. Keep work in progress, repair, rejects, shade holds, test specimens, approval samples and unpaid spares in separate status rows. A knitted panel or unfinished garment is not a shipped SKU.
Acceptance sampling and quantity reconciliation answer different questions. ISO 2859-1:2026 provides AQL-indexed sampling schemes for deciding lot quality from inspected samples; it does not count every unit or grant a shipment-quantity tolerance. Use inspection results to decide conformity, then reconcile the actual accepted count against every PO line.
Use a pre-final quantity checkpoint
Request a SKU status report before final packing: ordered, knitted, assembled, finished, passed, repair, rejected and remaining. Review it early enough to make replacements without delaying the booked shipment. Investigate directional shortages—such as repeated losses in one large size or one color—instead of averaging them away.
If a shortage cannot be recovered, the supplier should propose a written disposition showing affected SKU, cause, recoverable date, cost and document changes. The buyer can approve partial shipment, revised quantity, replacement timing or another contractual remedy. Silence is not approval.
Reconcile carton assortments to the SKU total
Define solid-size or mixed-size cartons, units per carton, ratio sequence, carton count, residual-carton method, gross and net weight fields, carton dimensions and marks. For mixed packs, write the exact assortment—for example, a named unit count by size—rather than “standard ratio.”
Add every carton line and compare it with the final SKU count. Then compare the packing list, commercial invoice, shipping instruction and warehouse advance notice. An accurate order total can still fail receiving when a carton label says one size and contains another.
Control substitutions and last-minute transfers
Do not let production move quantities between sizes, colors, destinations or label versions without named buyer approval. Record the old quantity, new quantity, reason, affected materials, price, delivery and document revision. Update all downstream files from one approved change record.
When goods are repaired or repacked, preserve their original SKU identity and inspection status. Reinspect the affected characteristic and recount the changed cartons. Avoid copying yesterday's packing list after a late replacement or carton split.
Close the order with a variance report
After release, compare ordered, approved revised, shipped, invoiced and received quantities by SKU. Record unexplained differences, damaged or missing cartons, replacements and credits. This closeout distinguishes manufacturing variance from freight or warehouse variance and improves the next production allowance.
Keep the report with PO revisions, approvals, inspection results, packing lists and carton evidence. For replenishment, update the commercial size mix from sales and receiving data; do not silently turn one production shortage into the next order's forecast.
Buyer quantity-control checklist
- Every style-color-size-destination combination has one SKU line.
- Ordered units and subtotals reconcile before material booking.
- Tolerance is exact or explicitly defined at a named level.
- Production allowance is not treated as delivery permission.
- Only accepted first-quality packed units count as deliverable.
- Samples, tests, repairs, rejects and reserves have separate status.
- Buyer approval is required for SKU redistribution.
- Carton assortments add back to every PO line.
- Packing list, invoice and shipping data use the final count.
- Shipped and received quantities are closed by SKU.
Yushengda's confirmed commercial MOQ is 100 pcs/color, subject to project feasibility; the exact size ratio and delivery tolerance still need project-specific agreement. The factory develops wool, cotton, acrylic, viscose, cashmere and blended knitwear across 3GG–16GG. Use the yarn-booking guide, the small-brand inventory guide, or send your color-size matrix, pack plan, quality requirements and delivery window for an RFQ discussion.
Primary references: GS1, Apparel and footwear, for standardized product identification across apparel variants; ISO, ISO 2859-1:2026, confirming that AQL-indexed acceptance sampling evaluates lot quality rather than performing a full shipment count. Competitor articles were reviewed only to identify common omissions; no tolerance, ratio, cases, images or wording were reused.