Set sweater needle and metal control before production by identifying every needle, pin, blade and metal-part risk; controlling issue and return; stopping work when a needle breaks; reconstructing all fragments; isolating affected work when any piece is missing; and defining validated detection, disposition and release records. The buyer must specify product scope and acceptance criteria—there is no universal detector setting for every sweater and trim combination.
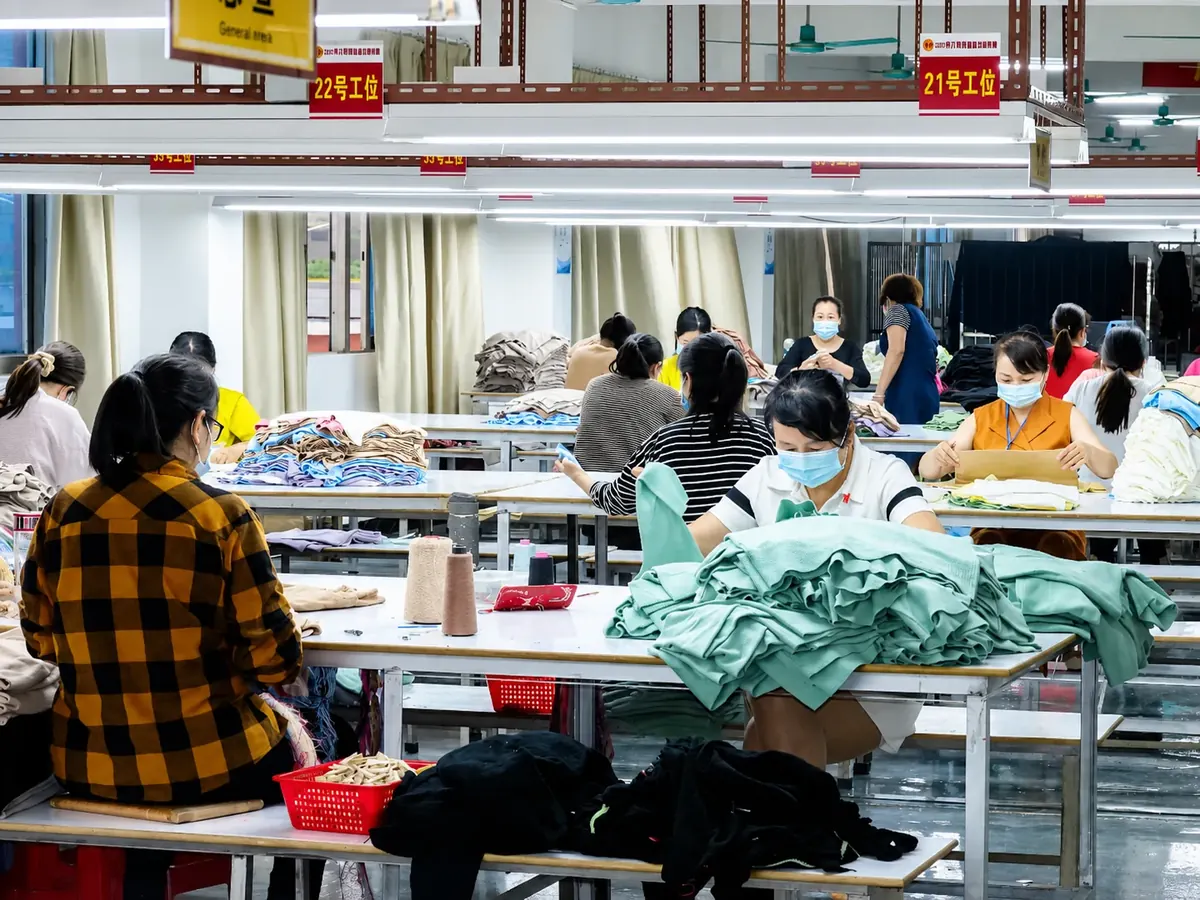
Start with the product hazard, not a certificate request
A broken sewing, linking, embroidery, hand-sewing or tag-gun needle can leave a sharp fragment in a garment. Pins, staples, blades, wires and damaged tool parts can create related risks. Map each operation and subcontracted process where a sharp or metallic object can contact panels, complete garments or packaging.
Destination-market law and buyer programs must be assessed separately. The US Consumer Product Safety Commission's current apparel guide notes that children's clothing is not technically within the cited sharp-point test scope, but clothing containing sharp points or edges may still be considered hazardous and can lead to recall action. Do not translate that statement into a claim that one detector result proves all legal compliance.
| Control layer | Question | Required evidence |
|---|---|---|
| Prevention | Which sharps enter each work area? | Inventory, issue/return and workstation rules |
| Breakage | Were all parts recovered? | Reconstructed needle and incident record |
| Containment | Which work may be affected? | Time, machine, operator, bundle and location trace |
| Detection | Can the selected system detect the target? | Named test piece, positions and verification log |
| Release | Who reviewed exceptions and cleared goods? | Signed disposition and shipment traceability |
Write one scope for every operation
List flat knitting, linking, overlocking or sewing, embroidery, hand attachment, repair, labeling, tag application, finishing, inspection and packing. Include outside processors. State which needles and sharp tools are allowed, who stores them, who issues replacements, and how damaged items are returned and counted.
Keep loose pins, staples and uncontrolled blades out of product areas where the buyer program prohibits them. Secure scissors, snips and tools where risk justifies it. A clean final detector record cannot explain an uncontrolled sharp that is not detectable by the chosen technology.
Stop, reconstruct and contain every breakage
When a needle breaks, stop the affected operation and prevent the garment, nearby work and waste from moving forward. Collect the fragments and compare the reconstructed pieces with a complete needle of the same type. Record date, time, machine or workstation, operator, style, color, size or bundle, operation and all pieces found.
If any fragment is missing, define the affected interval from the last verified good condition. Isolate work in progress, garments, floor sweepings, machine area and containers that could contain the piece. Search using an approved method, document the result, and authorize disposition. Never replace the needle and restart while the missing-piece decision remains open.
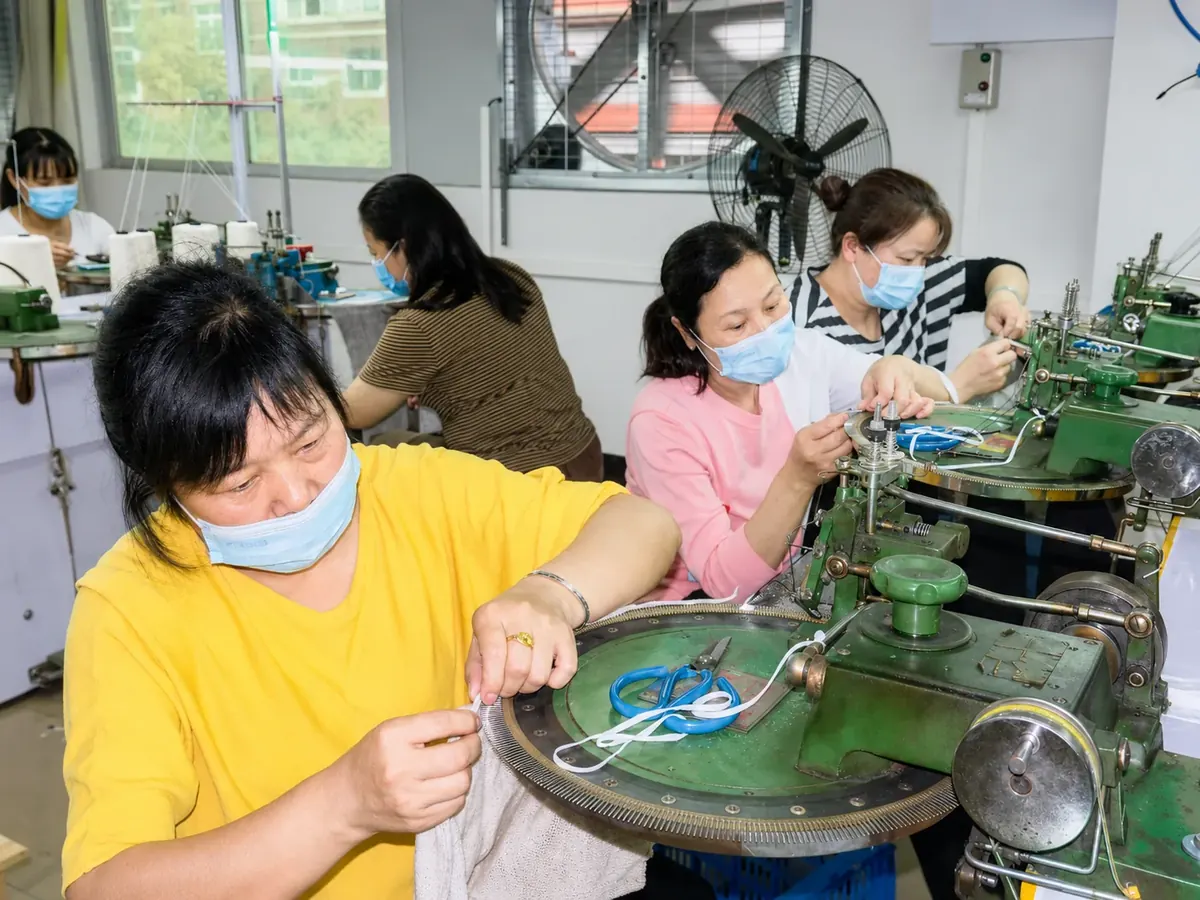
Do not confuse a needle detector with every-metal detection
Detection capability depends on the equipment principle, target material, target size and orientation, aperture, garment thickness, speed, position and surrounding interference. HASHIMA's official needle-detector guide distinguishes magnetic needle detection from broader metal detection and explains that magnetic systems do not detect non-magnetic metals such as aluminum and copper. Confirm the target and technology instead of writing only “metal detected.”
Metal buttons, zippers, snaps, rivets, wires or decorative components can affect the route. Decide before production whether the product can pass through the selected system, needs a validated alternative, or requires separate component and area controls. Do not remove a functional metal trim solely to make a generic detector step easier.
Define performance with a named test piece
The buyer or responsible technical party should specify the approved detector type, test-piece material and dimension, required sensitivity, test positions, challenge frequency, product presentation and failure response. Sensitivity numbers are not comparable without this context. Never copy a value from another factory, brand or garment category.
Challenge the effective detection area at defined positions rather than checking only the belt center. Verify at startup, after relevant interruption or adjustment, at defined production intervals and at the end of a lot according to the agreed program and equipment instructions. Record each result and keep failed-check products on hold back to the last successful verification.
Build a controlled detection and packing zone
Separate unchecked, passed, failed and rechecked goods physically and by status. Prevent a passed garment from returning to an uncontrolled needle or staple area. Control personal metal objects and loose tools where they could cause alarms or contaminate product. Keep the detector clean, stable and operated by trained, authorized staff.
Mark cartons or production records only after the complete quantity has followed the approved route. If a garment alarms, quarantine it; locate and identify the cause under the procedure; document repair, rejection or reinspection; and check whether the event signals a wider lot or process problem.
Audit records for traceability, not decoration
Review needle stock and issue/return balance, broken-needle records with retained fragments where required, missing-fragment investigations, maintenance and verification logs, detector challenge results, alarm and reject records, operator training, subcontractor controls and final quantity reconciliation.
A report should identify the PO or style, product category, colors or lots, date, equipment, agreed test piece and criteria, quantity checked, rejects, rechecks, exceptions and release authority. A photograph of garments on a conveyor does not establish that the defined sensitivity remained effective throughout the lot.
Connect metal control to final inspection
Treat any confirmed sharp fragment as a safety issue requiring the agreed critical-defect and escalation route. Final AQL inspection may verify records and sample products, but sampling alone does not replace a buyer requirement for 100% detection. Conversely, 100% passage through a detector does not replace visual workmanship, trim, measurement or other safety checks.
Before shipment, reconcile packed quantities with pass status, investigate every open incident and confirm that reworked goods re-entered the approved route. Retain records for the period required by the buyer, law and company policy, with access linked to the shipment.
Buyer needle-control checklist
- All internal and subcontracted sharp-object operations are mapped.
- Needle and tool issue, return and replacement are controlled.
- Breakage stops work and all fragments are reconstructed.
- Missing fragments trigger defined isolation and search.
- Target metal and detector technology are compatible.
- Metal trims have a documented product-specific route.
- Test piece, sensitivity, positions and frequency are named.
- Failed verification holds goods to the last confirmed pass.
- Checked and unchecked goods cannot be mixed.
- Shipment release closes incidents and reconciles quantity.
Yushengda develops custom knitwear in wool, cotton, acrylic, viscose, cashmere and blends across 3GG–16GG, subject to the project. Needle and metal-control requirements must be confirmed for the actual buyer program and product. Use the AQL inspection-plan guide, the trim approval guide, or send your product category, market, trims, process map and quantity for an RFQ discussion.
Primary references: US CPSC, Guide to US Apparel and Household Textiles, including its sharp-point discussion for children's clothing; HASHIMA, Needle Detector Guide Book, explaining detector principles, test pieces and detection limitations. Industry and competitor articles were used only to identify coverage gaps; no proprietary settings, cases, images or wording were reused.